

 English
 中文简体
 русский
Industry news
 Home / News / Industry news / HDPE Pipe Fittings Types: A Complete Guide to Connections, Sizing & Selection
HDPE Pipe Fittings Types: A Complete Guide to Connections, Sizing & Selection
 2026.09.14
 Industry news
Short answer: HDPE pipe fittings are divided by connection method and by function. The connection method includes butt fusion, electrofusion, socket fusion, threaded, compression and flanged types. The function category covers elbows, tees, reducers, end caps, flanges and adapters. A factory-floor understanding of both dimensions is what separates a smooth installation from a site rework.
Standing in a warehouse with pallets of HDPE fittings, the challenge is not whether the parts are good — it is whether the team has matched the right fitting type to the right pipe, pressure class and job site condition. As a manufacturer that has produced HDPE piping components since 2002, we have seen the same confusion on projects all over the world: electrofusion couplings sitting next to butt fusion reducers, threaded adapters mixed with compression unions, and no one certain which one belongs on the water line.
This guide explains the different types of HDPE pipe fittings from a manufacturer's point of view — what each type is actually built to do, where it works best, what tolerances matter, and how to avoid expensive mismatches. This is practical classification, not just a list of names.
What Are HDPE Pipe Fittings and Why the Classification System Matters
High-density polyethylene (HDPE) pipe fittings are injection-moulded or fabricated components that connect, terminate, reduce, divert or control the flow in a polyethylene pipeline. Unlike metal fittings, HDPE fittings are designed to be joined to the pipe itself — often by melting the two surfaces together — which means the fitting becomes part of a continuous, leak-free pipe wall.
The classification of HDPE pipe fittings is not academic. Installers, purchasing teams and project engineers need a reliable mental model to answer three questions:
- How will the fitting be joined to the pipe?
- What hydraulic or directional function does the fitting serve?
- What pressure rating and dimension standard apply to the system?
Get the first question right, and the installation crew knows which machine or tool to bring. Get the second right, and the pipeline layout functions as designed. Get the third right, and the system will not fail at a weld or a threaded joint. The rest of this guide follows that logic.
Six Connection Methods: The First Dimension of HDPE Fitting Types
The single most important way to classify HDPE pipe fittings is by how they connect to the pipe. HDPE does not get solvent-cemented like PVC, and it is not usually threaded for pressure piping (although threaded HDPE fittings exist for low-pressure and transition applications). Instead, HDPE relies on six practical connection families.
1. Butt Fusion Fittings
Butt fusion is the most widely used joining method for HDPE pipes above 63 mm. The pipe ends and the fitting ends are clamped in a fusion machine, faced flat, heated against a heater plate at around 200–210 °C, then pressed together under controlled force. The result is a monolithic joint — the fitting and pipe become one continuous piece of polyethylene.
Our butt fusion fitting series covers elbows, tees, reducers, equal and reducing couplings, end caps and flange adapters in diameters from DN63 to DN1200. These are the workhorses of municipal water, wastewater, gas and industrial lines.
Typical strengths
No elastomeric seals; chemical-resistant joint; long-term tensile strength; suited for buried and above-ground pipelines.
Limitations
Requires a butt fusion machine and trained operators; not practical for very small diameters (below DN20); difficult in trenches with tight working space.
2. Electrofusion Fittings
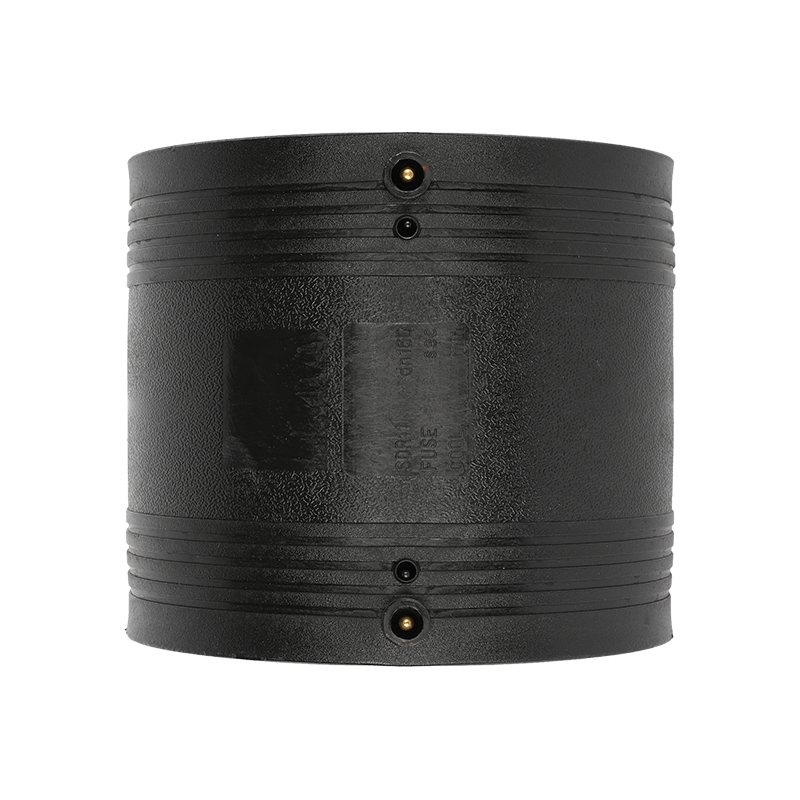
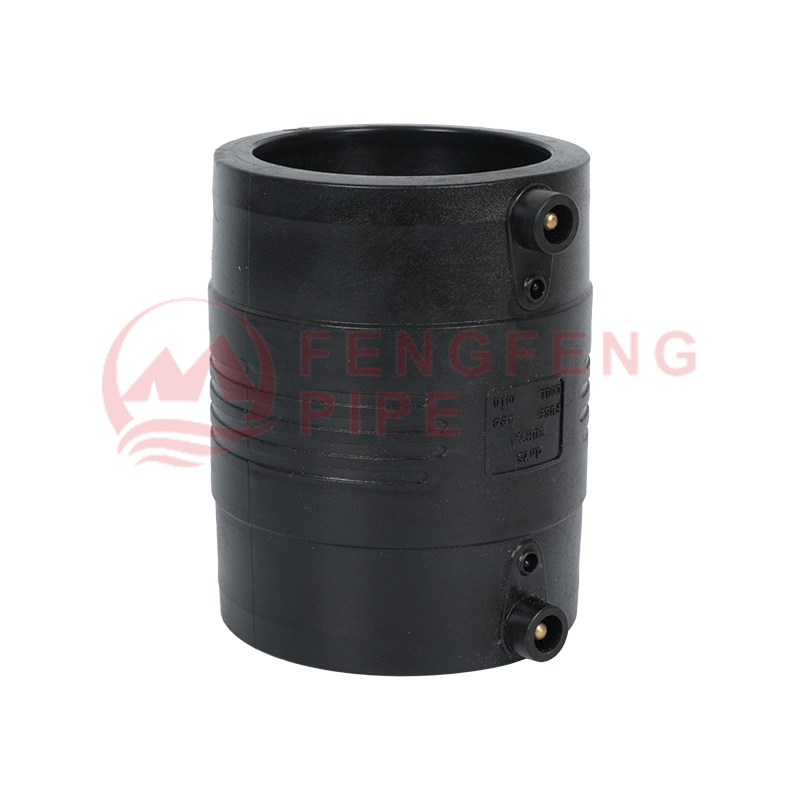
Electrofusion fittings have a metal resistance wire embedded in the socket or saddle. The fitting is clamped onto the pipe end, a special welding box sends current through the wire, and the polyethylene melts and fuses. Electrofusion is the preferred method for repair, for constrained spaces, and for diameters where carrying a large butt fusion machine is impractical.
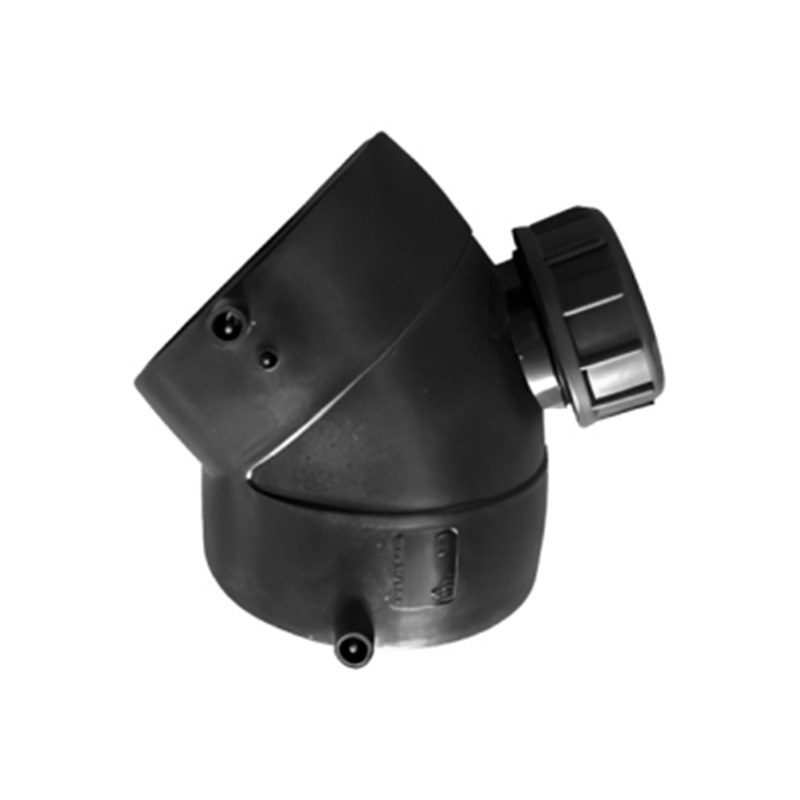
Our electrofusion series includes couplers, tees, 45° and 90° elbows, reducers, flange adapters, tapping saddles and end caps from DN20 to DN315. Electrofusion is also the safest method when the pipe is already buried and a new branch or repair coupling must be added.
3. Socket Fusion Fittings
Socket fusion is commonly used for small-diameter HDPE pipe (typically DN16–DN110). The outside surface of the pipe spigot and the inside surface of the socket are heated with a socket fusion tool, then pushed together and held until cool. It is quick, requires simple equipment, and is very reliable in clean conditions.
Our socket fusion series covers couplings, elbows, tees, unions and adapters for small-bore HDPE pipe, frequently used in compressed air systems, water treatment dosing lines and aquaculture piping.
Which thermal fusion method should you choose?
Choose butt fusion when:
- Pipe diameter is above DN63
- Long straight runs need maximum joint strength
- A fusion machine can be positioned at the joint
- Pressure class is PN10 or higher
Choose electrofusion when:
- Working space is too tight for a butt fusion machine
- The pipe is already installed, e.g. repair work
- Branch connections or saddle fittings are needed
- Automated welding quality control is required
Choose socket fusion when:
- DN16–DN110 small-diameter pipe
- Fast manual installation without heavy machinery
- Workshop fabrication or confined trench work
- Low-cost connection for non-critical services
4. Threaded HDPE Fittings
Threaded HDPE fittings are used where a polyethylene line must connect to a metal, brass or PVC threaded component — for example, a gate valve, a water meter or a pump discharge. There are all-HDPE threaded fittings and metal-insert threaded fittings. HDPE threads are not as strong as metal threads per engagement, so these fittings are typically rated for lower working pressure than a fused joint.
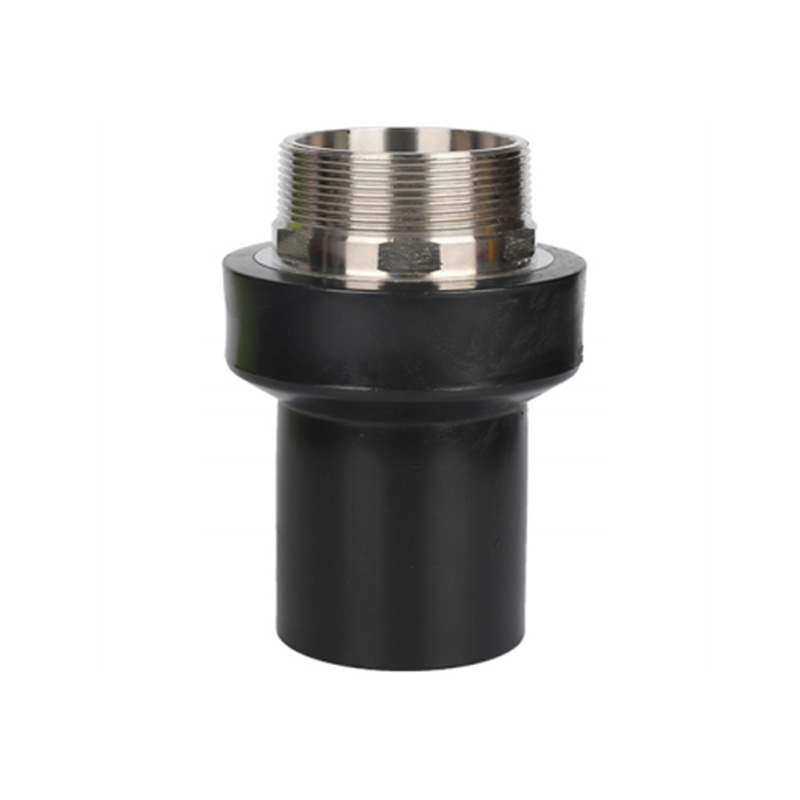
The company's HDPE threaded fitting series includes male and female adapters, elbows, tees, unions and couplings. The separate butt-threaded fittings series combines a fused socket or spigot end with a threaded end, giving installers the best of both worlds: a fused polyethylene connection on the pipe side and a threaded transition on the equipment side.
Good to know: When joining threaded HDPE fittings to metal, always use thread seal tape or a suitable thread compound. Do not over-torque the HDPE fitting — the thread root can crack, and that failure may not be visible until the line is pressurised.
5. Compression Fittings
Compression fittings grip the outside of the HDPE pipe with an O-ring seal and a compression nut, no heat required. They are a practical choice for temporary connections, for poly pipe in rural water supply, for drip irrigation, and for situations where an open flame or welding machine is not allowed on site.
Our PE/PP compression fitting range covers couplings, elbows, tees, end caps, and transition adapters in metric and inch sizes. Because the seal relies on the O-ring and the grip ring rather than a fused interface, compression fittings are easy to remove and reuse — a useful property in maintenance and seasonal installations.
6. Flange Adapters and Flanged Connections
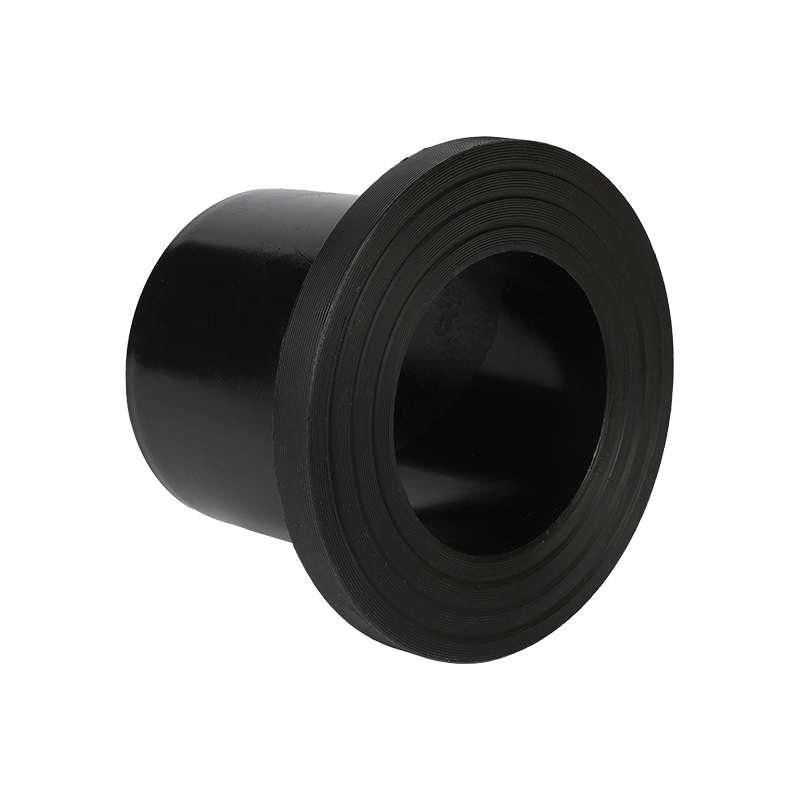
Flange adapters are butt-fused or electrofused onto the HDPE pipe, then a loose backing flange (usually steel or ductile iron) is used to bolt the assembly to a valve, pump or another flange. Flanged connections matter when components must be disassembled for maintenance, when connecting HDPE pipe to above-ground equipment, or when an HDPE line must tie into an existing flange network.
A flanged joint is inherently less strong in tension than a fused joint, but the ease of dismantling often outweighs that concern in pump stations and valve manifolds.
| Connection type | Typical size range | Equipment needed | Joint strength | Best application |
|---|---|---|---|---|
| Butt fusion | DN63–DN1200 | Butt fusion machine | Highest, monolithic | Municipal water, gas, industry |
| Electrofusion | DN20–DN315 | Electrofusion welding box | High, monolithic | Repairs, tight spaces, branches |
| Socket fusion | DN16–DN110 | Socket fusion heater | High, monolithic | Small-bore piping, workshop |
| Threaded | DN20–DN110 | Wrench, thread seal | Medium, pressure limited | Transition to metal valves/pumps |
| Compression | DN20–DN160 | Spanner, cutting tool | Medium, seal dependent | Irrigation, temporary or reusable joints |
| Flanged | DN50–DN600 | Bolts, gasket, torque wrench | High in compression, bolted | Valves, pumps, removable connections |
Standard Fitting Geometries: The Second Dimension
Once the connection method is set, the second dimension of HDPE pipe fitting types is geometry — the shape and hydraulic function. Every HDPE pipeline uses a predictable set of fitting geometries, and understanding their naming conventions avoids ordering errors.
Elbows — Direction Change
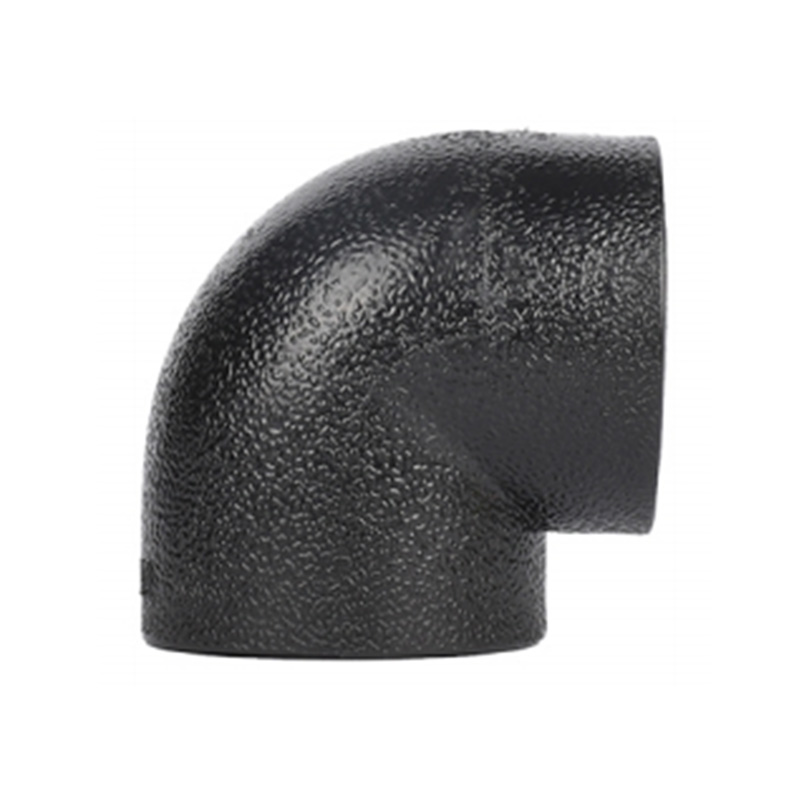
Elbows divert flow at a defined angle. The standard angles are 90°, 45° and 22.5°. Long-radius elbows are preferred for high-flow or slurry applications because they reduce pressure loss and wear. Factory-made HDPE elbows are available in equal-diameter form and in reducing form, the latter, for example, from DN160 to DN110.
Tees — Splitting or Combining Flow
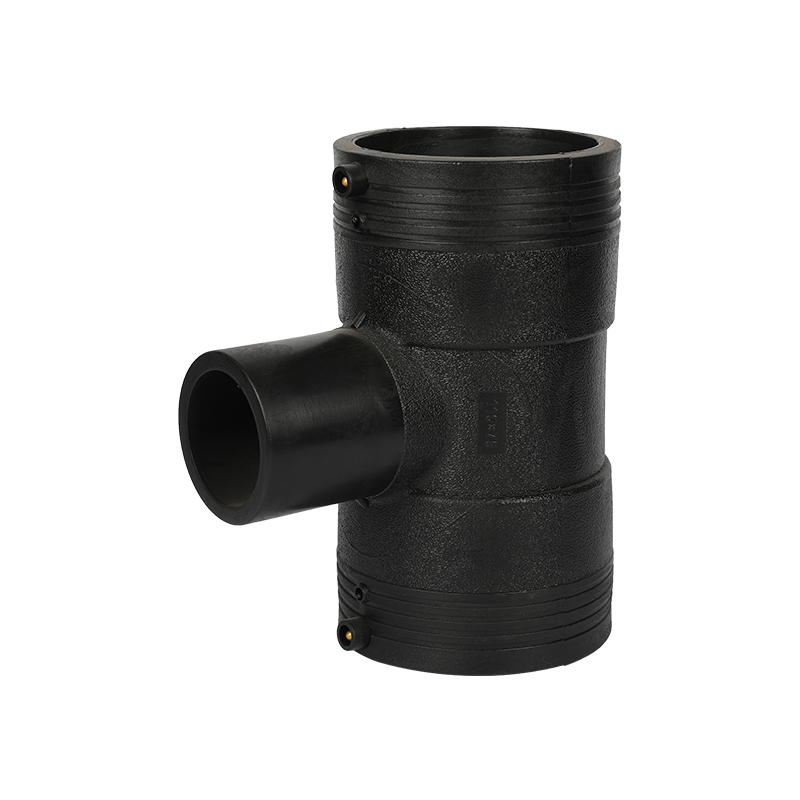
Tees have two outlets in one axis and one perpendicular side outlet. They exist as equal tees (all three ends the same diameter) and reducing tees (the branch or run is a smaller diameter). In newer PE100 pipe systems, injection-moulded tees are often preferred over fabricating a tee from cut pipe and saddle fittings because the moulded part has a more predictable stress distribution.
Reducers — Diameter Transition
Reducers connect one pipe diameter to a smaller one. They can be concentric — the axes of the two diameters align — or eccentric — the outer surfaces align. Eccentric reducers are common in pump suction lines to prevent air pockets. A reducer can be injection-moulded as a single piece or fabricated from larger pipe, but moulded reducers are stress-relieved and more reliable in pressure service.
End Caps — System Termination
End caps close the end of an HDPE line. They are available for every connection method — butt fusion, electrofusion, threaded and compression. An end cap must be rated for the same pressure class as the pipe, and in larger diameters, an end cap may need to be supported. In temporary pipeline works, a threaded or compression end cap is useful because it can be reopened.
Flange Adapters — Connecting to Flanged Components
As described earlier, flange adapters are fused to the HDPE pipe and provide a flat face for a loose backing flange. Their geometry matters in flange alignment: if two flange faces are more than a few millimetres out of parallel, bolt stress concentrates and the gasket can extrude.
Unions — Quick Disconnection
HDPE unions allow two pipe sections to be disconnected without cutting the pipe. They are widely used upstream of filters, pumps and flow meters. In buried pipelines, unions are usually avoided because the elastomeric seal can have a shorter service life than a fused joint.
Adapters and Transition Fittings
Adapters connect HDPE pipe to other materials — PVC, steel, copper or ductile iron — or to different end types, such as female threads, male threads, or a flange. When the pipeline must transition from HDPE to PVC, use a proper transition fitting rather than a generic threaded adapter; this prevents the mismatch between polyethylene's thermal expansion and PVC's stiffness.
| Fitting type | Function | Typical sizes (DN) | Common sectors |
|---|---|---|---|
| 90° elbow | Direction change | 20–1200 | Water, drainage, gas, industry |
| 45° elbow | Gentle direction change | 20–1200 | Buried pipelines, cable ducting |
| Equal tee | Branched flow | 20–630 | Water distribution, irrigation |
| Reducing tee | Branched flow to smaller line | 25×20–630×315 | Water supply networks |
| Concentric reducer | Diameter reduction | 25×20–630×315 | Pump stations |
| Eccentric reducer | Diameter reduction, avoid air pockets | 25×20–630×315 | Pump suction lines |
| End cap | Line termination | 20–1200 | Culvert ends, future extensions |
| Flange adapter | Bolted connection | 50–600 | Valves, pumps, above-ground plant |
| Male/female adapter | Threaded transition | 20–110 | Meters, brass valves, taps |
| Union | Removable joint | 20–110 | Filters, pumps, maintenance points |
Valves as Fittings?
Valves are technically flow-control devices, but in any HDPE piping system, they are ordered together with fittings and installed between two fitting connections. Gate valves, butterfly valves and ball valves are produced with HDPE or flange ends to integrate directly into polyethylene lines. We include valves in our product range because a project buyer should be able to source the complete connection package — pipe, fittings and valves — from one manufacturing partner.
How to Choose the Right HDPE Pipe Fitting: A Selection Framework
Now that both classification dimensions are clear, selection becomes a five-step process. These steps are the same ones our technical team applies when a customer sends a request with a pipe specification but no fitting list.
Step 1: Define the pressure class
The pressure class of the pipe and fittings is expressed either as PN (nominal pressure in bars) or through the SDR ratio — the pipe outer diameter divided by wall thickness. A lower SDR means a thicker wall. For example, SDR11 pipe has a wall thick enough for PN16; SDR17 corresponds to approximately PN10. The fitting must have the same SDR class as the pipe. Using a lower SDR (thicker) fitting on a higher SDR (thinner) pipe can create stress concentration at the transition.
Figure 1 — Common HDPE SDR / PN correlations
Lower SDR = thicker wall = higher pressure rating. Always order fittings from the same SDR series as the pipe.
Step 2: Match the dimension standard
HDPE pipe is produced in metric (ISO 4427 / EN 12201) and inch or iron pipe size (IPS) series. A metric DN110 pipe has an outside diameter of 110 mm; an IPS 4" pipe has an outside diameter of 114.3 mm. These two sizes are not interchangeable. A fitting designed for 110 mm pipe will not seal or fuse correctly on a 114.3 mm pipe. Always confirm the outer diameter of the pipe before ordering fittings.
| Nominal metric size | Metric OD (mm) | IPS size | IPS OD (mm) |
|---|---|---|---|
| DN90 | 90 | 3" | 88.9 |
| DN110 | 110 | 4" | 114.3 |
| DN125 | 125 | — | — |
| DN160 | 160 | 6" | 168.3 |
| DN200 | 200 | 8" | 219.1 |
Step 3: Select the connection method by site conditions
Ask three questions. First, can a fusion machine physically reach the joint? If not, use electrofusion or mechanical compression. Second, will the joint need to be dismantled in the future? If yes, flange or compression connections are necessary. Third, what is the maximum pressure transient, including water hammer? Fused joints are the only type that achieves the full pressure rating of the pipe, while threaded HDPE fittings typically have a lower pressure limit.
Step 4: Consider the fluid and environment
HDPE is resistant to a very wide range of chemicals, but some fluids — strong oxidising acids, certain hydrocarbons and chlorinated solvents — may cause stress cracking in polyethylene, especially at elevated temperatures. Check the chemical compatibility and the operating temperature. PE100 material extends the allowable pressure range compared with PE80. At temperatures above 30 °C, the pressure rating must be derated; above 60 °C, polyethylene pipe systems shift into a specialised regime such as PE-RT II, which is designed for high-temperature applications.
Step 5: Buy from a single responsible supplier
When a project uses pipes from one manufacturer and fittings from another, warranty claims are difficult and dimensional mismatch is possible. A manufacturer that produces both pipe and fittings, and can certify that both are made from compatible PE material with consistent melt flow index, removes a significant project risk.
Installation Quality: Seven Common Mistakes to Avoid
A well-made fitting still fails if installation rules are ignored. The following are the most frequent mistakes our technical support team has observed across hundreds of projects.
- Failing to clean the joint surface. Dirt, moisture and grease on the pipe spigot contaminate the melt. The standard requirement is a clean, dry surface; wipe with a lint-free cloth and avoid using solvents unless prescribed by the fitting supplier.
- Ignoring the heating time and temperature. Both under-heated and overheated joints look similar until pressurised. Use the welding machine's calibrated cycle and record the parameters for traceability.
- Moving the joint during the cooling phase. Polyethylene crystallises slowly. Moving, pushing or loading the joint before the specified cooling time creates internal stress that can lead to ductile failure years later.
- Using the wrong sized socket or spigot. A 110 mm electrofusion fitting must never be forced onto a 114.3 mm pipe. Even a small mismatch of 0.5 mm can create voids in the fusion zone.
- Over-torqueing threaded HDPE fittings. The practical rule: one hand on the wrench, not two. Metal threads deform HDPE threads at a fraction of the torque that a metal fitting would withstand.
- Not supporting vertical runs. HDPE creeps under continuous load. Vertical HDPE lines with heavy valves need appropriate anchors and supports to prevent tensile stress at the fittings.
- Skipping pressure testing before backfilling. Test the assembled line at 1.5 times the working pressure before covering the trench. A joint that leaks at that pressure would have failed in service anyway, and it costs far less to fix when the trench is open.
Factory perspective: We test fittings and pipes in our own production line, but the final joint is made by the installer. That is why we include clear welding parameter sheets with every shipment and encourage customers to request a free installation training session before the project begins.
Real-World Applications by Industry
The choice of HDPE pipe fitting types depends heavily on the end-use sector. Each sector prioritises a different combination of connection method and fitting geometry.
Municipal water supply
Butt fusion and electrofusion dominate. Pressure class PN10–PN16, SDR17 or SDR11. Elbows, tees and reducers are the essential geometry. Flanged connections appear at pump stations and valve chambers.
Agriculture and irrigation
Compression fittings and threaded fittings are common for small-diameter lines up to DN63. Electrofusion is used for the mainline network. Fittings that can tolerate UV exposure and occasional impacts from farm machinery are a practical requirement.
Marine aquaculture
Polyethylene is the standard choice for marine cage systems and seawater intake lines, because saltwater has little effect on PE. The special pipe support brackets and frame connectors we produce for floating cage structures require fittings engineered for cyclic wave loading. Socket fusion and butt fusion are used to assemble the pipe frames.
Building drainage and rainwater systems
Siphon drainage fittings, which are our dedicated product line, rely on precisely sized reducers, offsets and pressure-tight joints. HDPE fittings in building services are often welded with socket fusion or electrofusion because these methods allow installation near existing structures without hot works.
Industrial processing
Chemical and mining pipelines demand the highest material quality: PE100 with SDR11 is the typical baseline. Butt fusion is almost mandatory because it produces the smoothest inner bore and the highest joint strength, minimising pressure loss and leak risk.
Gas distribution
Gas lines require PE80 or PE100 black pipe with yellow stripes or a fully yellow pipe. Electrofusion fittings are widely used because the welding process parameters are easily logged and certified. Traceability of every fitting — date, batch, machine and welder ID — is part of the regulatory framework in many countries.
Manufacturer's Checklist for Ordering HDPE Pipe Fittings
When you send an enquiry to a factory, the best response comes from a clear specification. Use this checklist to make sure nothing is ambiguous.
- Pipe material grade: PE80 or PE100?
- Outside diameter standard: metric ISO or IPS in inches?
- SDR / pressure rating: e.g. SDR11 PN16, SDR17 PN10
- Connection type: butt fusion, electrofusion, socket fusion, threaded, compression or flange
- Geometry: elbow degrees, equal or reducing tee, concentric or eccentric reducer, end cap, union, adapter
- Quantity per item: with a clear size break-down
- Colour: black, black with blue stripes, blue, orange or yellow
- Certification: ISO 9001, ISO 14001, product test reports and batch certificates
- Packaging and marking: carton, pallet, printed designations on each fitting
As a manufacturer with more than two decades of extrusion and injection moulding experience, we recommend against searching only for the cheapest quote. Dimensional consistency — the outside diameter tolerance of both the pipe and the fitting socket — determines whether the joint will fuse correctly over a full production run, not just on one sample from the top of a pallet.
Frequently Asked Questions
What are the different types of HDPE pipe fittings?
HDPE pipe fittings are grouped in two ways. By connection method: butt fusion, electrofusion, socket fusion, threaded, compression and flanged. By geometry: elbows, tees, reducers, end caps, flange adapters, unions and adapters. Each type serves a specific installation condition and pressure requirement.
How do I know which HDPE fitting connection method to use?
Match the method to the working environment and joint requirements. For long buried pipelines, use butt fusion. In tight trenches or for repairs, use electrofusion. For small-bore industrial lines, socket fusion is fast and reliable. Use threaded fittings for transition to metal equipment, compression fittings where joints must be dismantled, and flange adapters at valves and pumps.
Can HDPE fittings be connected to PVC or metal pipes?
Yes, but only through transition fittings. Threaded adapters, flanged adapters and compression fittings are the safe ways to join HDPE to PVC, steel or ductile iron. Do not glue or solvent-weld HDPE to PVC; the materials and curing behaviour are incompatible.
What is the difference between SDR11 and SDR17 fittings?
SDR11 fittings have a thicker wall and are rated for a higher pressure — normally PN16. SDR17 fittings are rated for about PN10. Both are made from the same HDPE material, but the SDR class must always correspond to the pipe class on the same line, because a mismatch changes the stress distribution at the fused joint.
Are electrofusion fittings stronger than butt fusion fittings?
Both methods, when performed correctly, produce a joint that is at least as strong as the pipe itself. The difference is practical, not one of strength. Butt fusion is the most economical for straight runs of large-diameter pipe; electrofusion is more practical when you are welding a branch or a repair where a butt fusion machine cannot be positioned.
How long do HDPE pipe fittings last?
The service life of HDPE pipe fittings is generally stated as 50 years or more when the system operates within its rated pressure and temperature. The fitting material, the fusion joint quality and the operating stress together determine the actual life. Unrestrained threaded fittings, by comparison, have a shorter expected service life and are best used for access or maintenance points.
Can a threaded HDPE fitting be used on a high-pressure water line?
Threaded HDPE fittings have a lower pressure rating than fused joints. They are best used for transition connections at valves and meters, where the service pressure is below the rating stated by the fitting manufacturer. For high-pressure mains, use a flange adapter and a flanged valve instead of a threaded connection.
Where to Start on a New HDPE Piping Project
The correct approach to HDPE pipe fittings is not to memorise a catalogue but to understand the installation conditions, pressure rating and joint requirement for each location. Start by fixing the pipe specification — material grade, SDR class and outside diameter. Then move to the connection type, then the geometry, then create a line-by-line bill of materials.
For engineers and purchasing professionals who prefer to work directly with a factory rather than a trading company, the advantage is consistency: the same material because of a single raw material batch, controlled injection process, a clear incoming inspection standard and a single after-sales technical contact.
Whether the project is a rural water network using compression fittings across thousands of farm connections, a municipal DN800 pipeline with butt-fused reducers, or an offshore aquaculture installation requiring corrosion-free pipe frames and brackets, the classification system in this guide remains the same. Get the categories right, define the boundary conditions, and the product selection follows naturally.
KEEP IN TOUCH
About Us
Zhejiang Fengfeng Pipe Industry Co., Ltd. uses efficient single screw injection molding machines for high productivity and low energy use.
Products link
Contact
-

+86-19858193396
+86-13735359894 -

+86-0574-63555288
-

-

No. 21, Market Road, Diankou Town, Zhuji City, Shaoxing City, Zhejiang Province, China